Introduction
For decades, manufacturers ran plants on manual checks, paper logs, and end-of-shift reports. Production numbers arrived hours late. Quality issues surfaced only after defects had already shipped. Equipment problems were discovered when a machine stopped, not before.
That gap is exactly what Industrial IoT closes.
Manufacturers still hit the same blind spots:
- Limited visibility into equipment status
- Unplanned downtime
- Quality drift
- Reactive maintenance
- Inconsistent performance across lines and plants
Deloitte's 2025 Smart Manufacturing Survey found that 46% of large US manufacturers now use IIoT at the facility or network level. Connected operations have moved from experiment to expectation.
This guide covers what IIoT is, how it differs from consumer IoT and standard IT/OT setups, how the stack works end to end, where it pays off on the plant floor, and how to implement it without a rip-and-replace overhaul.
Key Takeaways
- IIoT connects industrial machines, sensors, software, and networks to collect and act on operational data
- Priorities center on uptime, safety, reliability, quality, and measurable performance gains, not consumer convenience
- Legacy and modern equipment can both connect through gateways, protocols, databases, and added sensors
- Successful rollouts start with one focused problem, then expand through validated use cases and secure integration
What Is Industrial IoT?
Industrial IoT, or IIoT, is an ecosystem that connects machines, controllers, sensors, software, and people across a manufacturing operation. The Industry IoT Consortium defines it as the integration of industrial control systems with enterprise systems, business processes, and analytics — so IIoT goes beyond connecting machines to the internet and turns physical events into decisions.
Think about what happens on a typical shop floor:
- A bearing starts vibrating outside its normal range
- A furnace drifts a few degrees off its process setpoint
- A conveyor logs a production count that doesn't match the work order

IIoT captures these events as data, in near real time, and routes them to the people and systems that need to act on them.
Basic machine connectivity just moves data from point A to point B. IIoT uses that data to trigger alerts, automate responses, flag maintenance needs, and improve quality, closing the loop between noticing a problem and fixing it.
IIoT sits inside the broader Industry 4.0 movement. NIST describes Industry 4.0 as the phase of manufacturing that joins physical production with smart digital technology, machine learning, and big data — with IIoT and smart manufacturing as core enabling pieces, not the whole strategy.
For manufacturers, the payoff is practical:
- Real-time visibility into what's happening on the floor
- Earlier identification of bottlenecks and root causes
- Better equipment utilization
- Tighter coordination between plant-floor teams and management
That is the gap Vistrian's Manufacturing Suite was built to close. FactoryLOOK pulls live data from equipment, sensors, and controllers into a single source of truth, so managers work from current numbers instead of yesterday's reports.
What Is the Difference Between IIoT, OT, and IT?
Two domains sit on either side of IIoT:
- Operational technology (OT): Monitors or controls physical processes directly — PLCs, SCADA systems, and machine controllers
- Information technology (IT): Manages business systems such as ERPs, email, databases, and analytics platforms
NIST notes these two worlds historically had different priorities. OT focuses on safety, production continuity, and preventing physical harm. IT focuses on data protection and business-system uptime.
IIoT is the bridge. It takes OT-generated data (machine states, sensor readings, process conditions) and connects it to IT-side applications like dashboards, analytics platforms, and reporting tools, so operational data informs business decisions instead of staying locked in a controller.
How Does Industrial IoT Work?
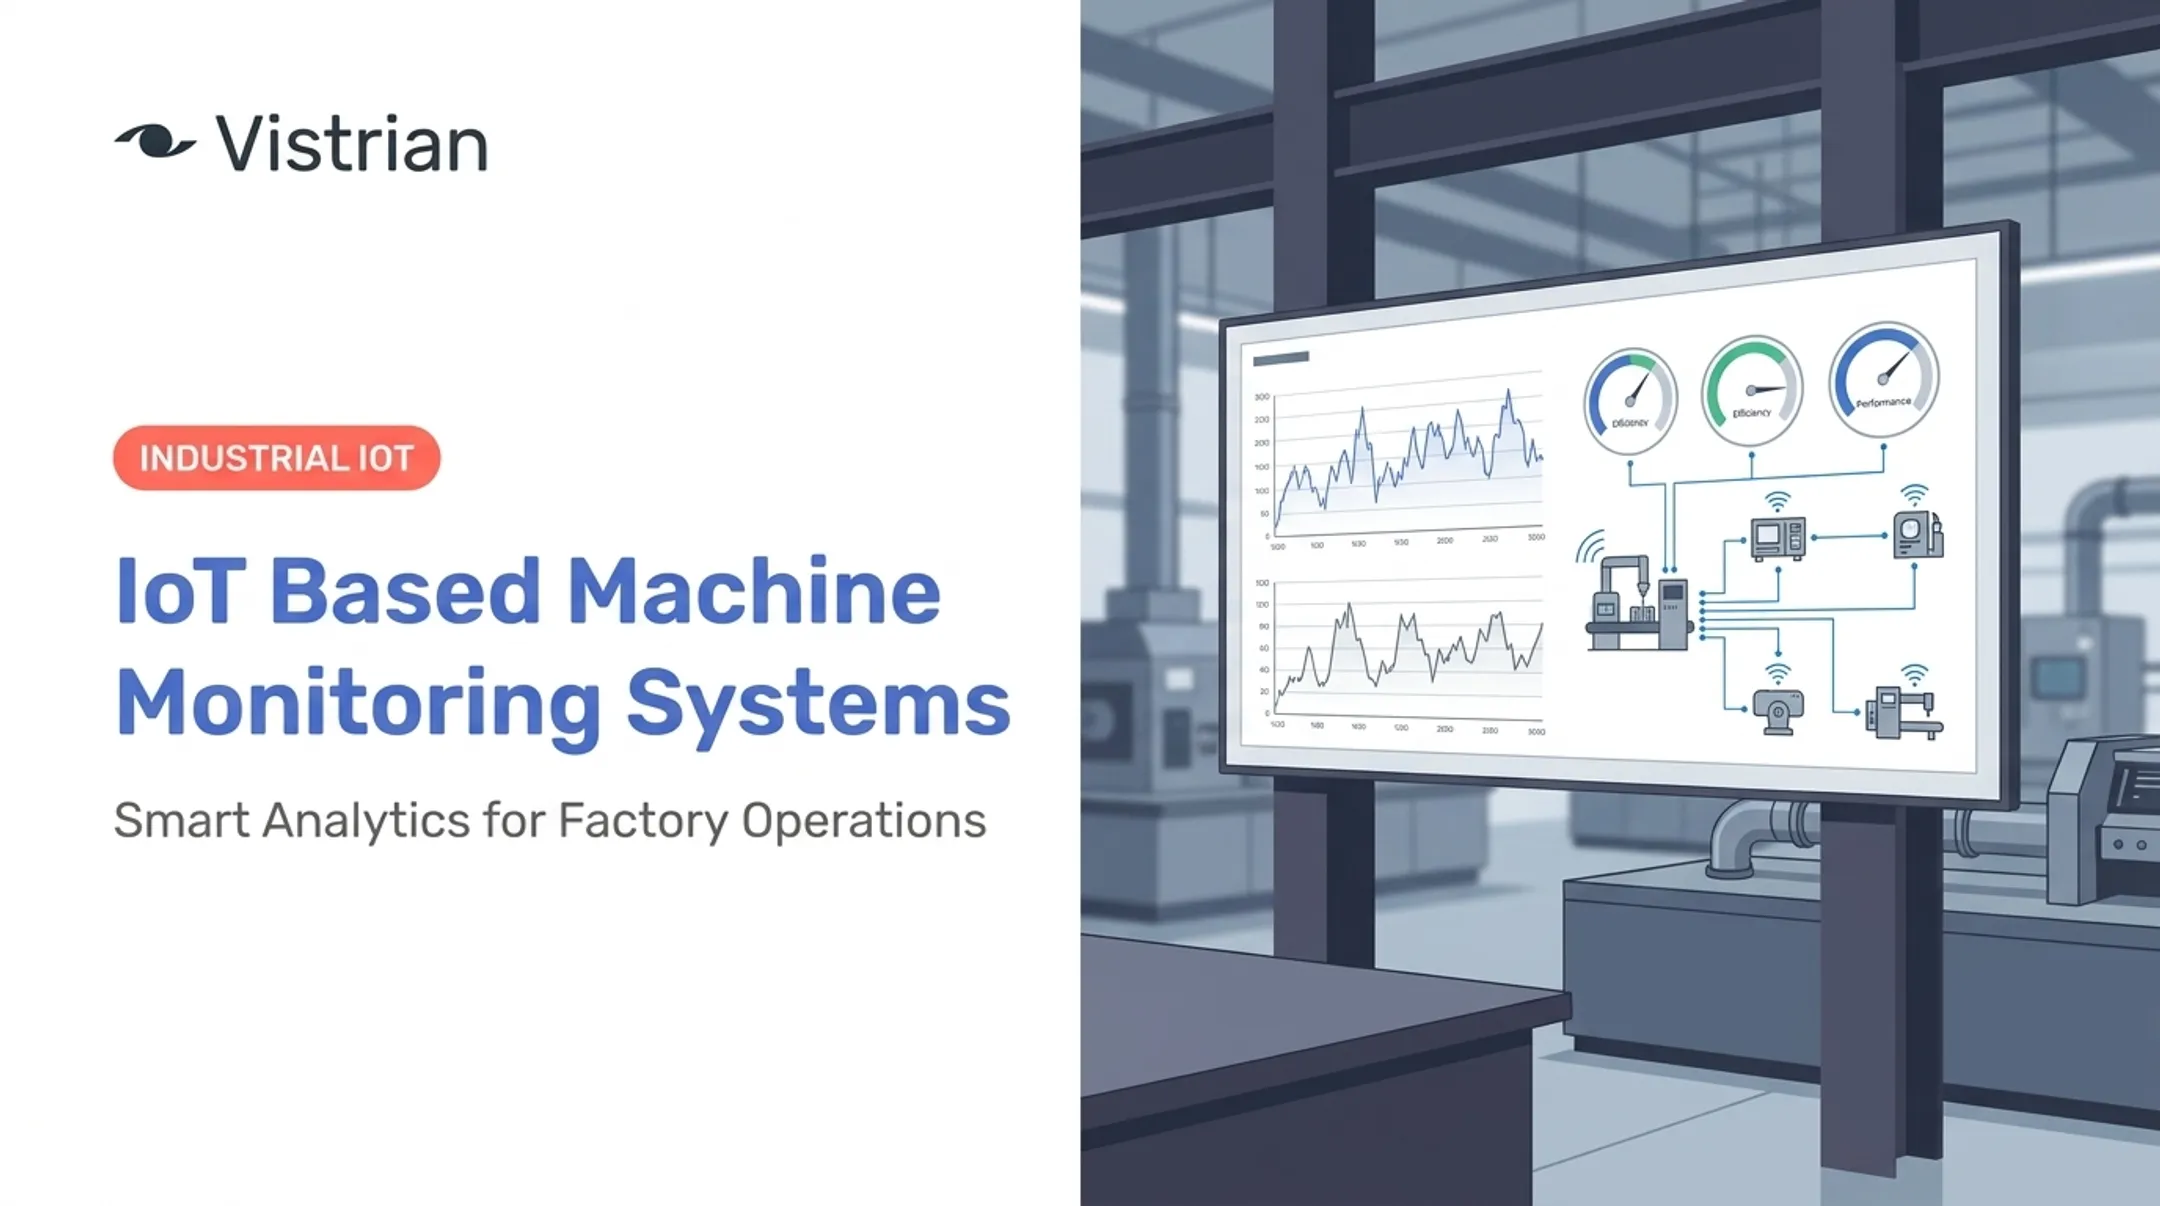
IIoT follows a fairly consistent data flow, regardless of industry:
- Sensors and machine interfaces capture measurements: temperature, pressure, vibration, energy use, machine state, production counts, quality indicators
- Gateways and connectivity devices translate signals from different controllers, protocols, and data formats into something a central system can use
- Edge or on-premises processing handles time-sensitive responses close to the machine
- Cloud or centralized platforms store data, run broader analytics, and support multi-site reporting
- Dashboards and alerts turn that data into something a supervisor or engineer can act on immediately

The hardest part of this chain is connecting equipment that was never built with connectivity in mind. Legacy machines, mixed-vendor controllers, and inconsistent databases are the norm on most factory floors, not the exception.
This is where a modular approach earns its keep. Vistrian's Manufacturing Suite, anchored by FactoryLOOK, connects directly to machine controllers, logs, and databases, and layers Vistrian Industrial IoT sensors on top for equipment that lacks a native digital interface. The result is a near-real-time feed covering machine health, process performance, and energy use. Teams can access it from a secure browser, phone, or tablet, on-premises or in the cloud.
Analytics is where raw data earns its value. Once machine and sensor data flows into a platform, analytics converts it into usable metrics:
- OEE, uptime, and utilization
- Throughput, yield, and cycle time
- Anomaly detection that flags failures before they cause a stoppage
Vistrian Analytics works alongside FactoryLOOK to catch early warning signals in equipment and processes. Teams get a window to act before a small deviation becomes a shutdown.
What Role Do Cybersecurity and Access Controls Play?
Connecting machines expands the attack surface. Every sensor, gateway, and network link is a potential entry point, and unlike a typical IT breach, an OT compromise can stop production or create a safety hazard.
NIST's Guide to Operational Technology Security (SP 800-82r3) lays out the baseline practices manufacturers should follow:
- Maintain a current asset inventory of every connected device
- Use secure communications and role-based access controls
- Segment OT networks from general IT traffic where appropriate
- Patch and monitor systems on a defined schedule
- Build an incident response process specific to OT environments
NIST also warns that active network scans, common in standard IT security, can destabilize sensitive OT devices or interfere with a running process. Passive monitoring is often the safer choice for the plant floor. Vistrian's approach reflects this reality: secure browser-based access and role-based dashboard views limit exposure without disrupting the equipment being monitored.
Industrial IoT Applications and Benefits
IIoT earns its budget line through a handful of high-value use cases. These are the applications where manufacturers see the clearest returns.
Predictive and condition-based maintenance replaces calendar-based schedules with equipment-driven ones. Instead of servicing a motor every 90 days regardless of condition, teams act when vibration or temperature data signals a developing problem.
McKinsey reports that predictive maintenance typically cuts machine downtime by 30% to 50% and extends machine life by 20% to 40%. VistrianMMS customers see similar results: IIoT sensor data and analytics catch failure patterns early, cut downtime in that same 30–50% range, and reduce emergency repair costs.

Real-time production monitoring and OEE give supervisors visibility they used to wait hours for. Machine-state data shows exactly where time is lost: a stalled changeover, a speed loss, or a recurring stoppage on line 3. FactoryLOOK surfaces cycle times, throughput, and equipment status as the shift runs, not in a report assembled afterward.
Quality and process control shift from spot checks to continuous monitoring. Deviations get caught as they happen, which supports statistical process control and tighter traceability between production data and quality records.
Remote and enterprise visibility matters most for leaders overseeing multiple plants. IIoT dashboards replace consolidated spreadsheets so teams can compare site performance and spot loss drivers in near real time, the problem Vistrian's Management Suite is built to solve.
Other common applications include:
- Energy monitoring tied to OEE and predictive-maintenance data
- Asset tracking and inventory visibility
- Connected robotics and automated material handling
- Worker safety alerts on hazardous processes
One concrete example: Blommer Chocolate's engineering manager reported that FactoryLOOK identified production bottlenecks, increased output potential, and helped the company avoid more than $1 million in unnecessary capital spending.
How Does IIoT Support Small, Mid-Sized, and Large Manufacturers?
Plant size shouldn't dictate whether IIoT is worth pursuing — it should dictate where you start.
- Smaller plants: Start narrow on one line, asset group, or recurring problem such as unplanned downtime
- Mid-sized manufacturers: Expand a single pilot into a standard approach across a few lines
- Large manufacturers: Use shared data models and centralized analytics for multi-plant monitoring
Vistrian's Manufacturing Suite is deployed across more than a dozen industries and over ten countries. Its modular structure lets a single-plant chocolate processor and a multi-site semiconductor operation both start small and scale on their own timeline.
Implementing IIoT in a Manufacturing Environment
The manufacturers who succeed with IIoT don't start with the technology. They start with a problem.
Begin with a defined operational issue, such as:
- Recurring, unexplained downtime
- Limited or delayed OEE visibility
- Reactive, calendar-based maintenance
- Quality variation without a clear root cause
- Difficulty comparing performance across sites
From there, a practical pilot follows a repeatable sequence:
- Select a specific asset or line for the pilot
- Define baseline KPIs before making any changes
- Identify the data sources needed — controllers, sensors, existing databases
- Confirm connectivity and assign clear data ownership
- Build dashboards or alerts and test them against real operating conditions
- Measure whether the pilot actually changed a decision or an outcome

Legacy equipment is usually the sticking point, not the software. Common barriers include:
- Mixed-vendor machines and missing digital interfaces
- Inconsistent naming conventions across assets
- Gaps between MES, CMMS, ERP, and historian systems
Vistrian Industrial IoT addresses this by adding sensors to machines that were never built with a digital interface, then syncing that data into FactoryLOOK with the rest of the plant. Western Digital reported smooth integration across varied equipment types and controllers. Soraa's systems architect noted easy integration with legacy fab tools and MES.
Once the pilot works, scaling brings a second set of requirements:
- Cybersecurity and network segmentation
- Data governance and user permissions
- Device management for sensors and gateways
- Integration standards across MES, ERP, and quality systems
- Training and change management for floor teams
On the return side, weigh implementation cost against a clear baseline:
- Downtime cost and current maintenance spend
- Throughput and quality losses
- Labor effort and avoided capital expenditure
Vistrian's Manufacturing Suite clients report an average payback period of less than one year. The Blommer Chocolate deployment alone projected over 20% OEE improvement alongside the capital expenditure it avoided.
Frequently Asked Questions
What is Industrial IoT?
Industrial IoT connects industrial assets, sensors, and systems to collect operational data for monitoring, analysis, automation, and better decisions. It is a core enabling technology within Industry 4.0 and smart manufacturing.
What are Industrial IoT solutions?
IIoT solutions stack connected sensors, machine interfaces, gateways, and networks with software platforms, analytics, and dashboards. That stack turns equipment and process data into actions manufacturers can take in real time.
What are some examples of Industrial IoT?
Common examples include predictive maintenance, real-time machine monitoring, OEE tracking, remote asset monitoring, connected robotics, quality monitoring, and supply chain visibility. Most manufacturers start with one use case, like downtime tracking, before expanding.
How is Industrial IoT different from IoT?
IIoT is the industrial application of IoT, built for reliability, safety, uptime, and scale rather than convenience. NIST notes that industrial IoT failures can cause production downtime and safety risks, while consumer IoT failures typically involve privacy or personal data issues.
What are the benefits of Industrial IoT?
Benefits include improved visibility, higher equipment utilization and uptime, better quality control, smarter maintenance planning, and faster decision-making. Manufacturers can also compare performance across lines, plants, or facilities in near real time.
What are the challenges of implementing Industrial IoT?
The most common hurdles are legacy equipment integration, cybersecurity, data quality, and workforce adoption. Proving ROI early—often through a focused pilot—usually determines whether a project scales or stalls.