Introduction
Walk any plant floor and you'll find the same scene: machine status on one screen, downtime logged on paper, quality data buried in a spreadsheet, and maintenance history living in someone's inbox. Nobody has the full picture.
That fragmentation costs real money. Teams spend hours reconciling reports instead of fixing problems. Warning signs go unnoticed until a machine is already down. Quality issues surface after the batch has already shipped.
IoT monitoring software solves this by collecting data from connected machines, sensors, gateways, and production assets—then organizing it so teams can protect uptime, quality, and throughput before small issues escalate.
This article covers how IoT monitoring works on the plant floor, which features separate a serious platform from a dashboard demo, common manufacturing use cases, and a practical framework for evaluating a system across one plant or many.
Key Takeaways
- IoT monitoring software turns scattered machine and sensor data into unified visibility on health, performance, quality, and maintenance risk.
- Evaluate platforms on legacy-equipment support, alert quality, and integration depth, not device count alone.
- The strongest platforms close the loop from raw telemetry to root-cause analysis and corrective action.
What Is IoT Monitoring Software?
IoT monitoring software collects, contextualizes, and presents data from connected equipment so manufacturing teams can identify problems and respond quickly. It's built for people running production, not just IT departments tracking network uptime.
Device Monitoring vs. Industrial IoT Monitoring
These terms get used interchangeably, but they answer different questions.
- Device monitoring checks whether a sensor or gateway is online, reporting data, and functioning correctly.
- Industrial IoT monitoring connects that same data to production output, maintenance schedules, quality outcomes, and business decisions.
The International Society of Automation defines industrial IoT as a connected network of sensor-based monitoring and production equipment and software that provides actionable information for better-informed decisions. Device monitoring tells you a sensor is alive; industrial monitoring tells you what to do next.
Core objectives of industrial IoT monitoring:
- Continuous visibility into machine and process conditions
- Early detection of abnormal behavior before it becomes downtime
- Remote oversight across shifts, lines, or plants
- Performance analysis tied to production metrics
- Predictive or condition-based maintenance planning
- Data-backed decisions instead of gut calls
Legacy equipment works too. A platform like Vistrian's FactoryLOOK connects to PLCs and PC-based controllers using standard industrial protocols, and pulls data from logs or databases when direct integration isn't possible. Machines that are decades old can still generate telemetry.
Who Uses This Data
Each role needs a different cut of the same data:
- Operators need real-time machine status and alarms
- Maintenance teams need historical trends and failure patterns
- Plant managers need throughput, downtime, and bottleneck data
- IT/OT teams need secure, auditable data flows
- Operations executives need cross-plant comparisons
How IoT Monitoring Software Works
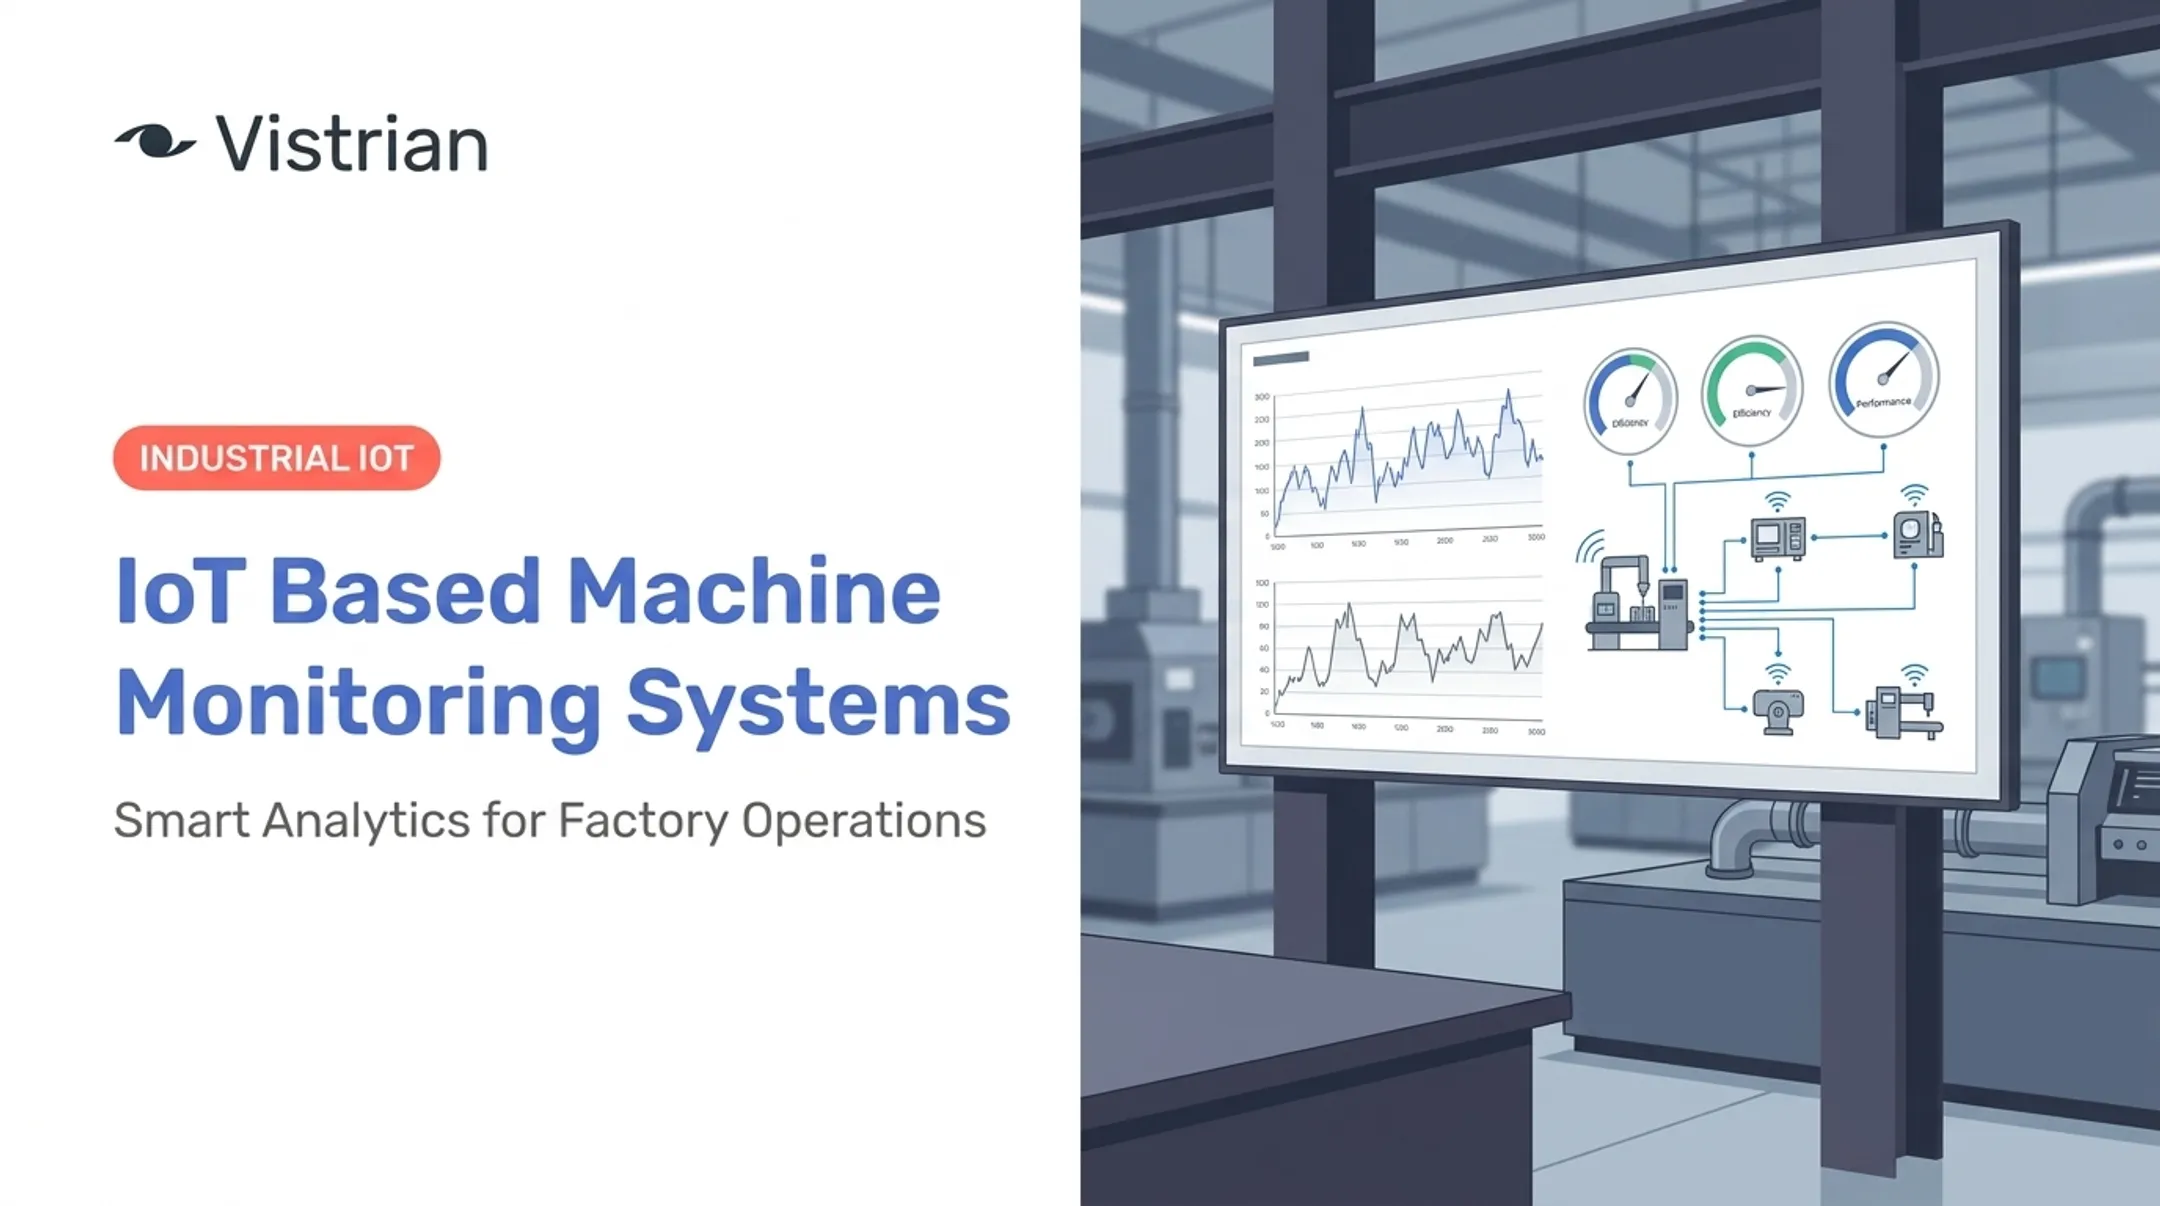
The workflow follows a consistent path: connect assets, collect telemetry, transmit and store the data, analyze it, then present it in a form someone can act on.
The Equipment and Sensor Layer
Every machine generates signals worth watching, but which ones matter depends entirely on the process. A CNC line cares about cycle time and spindle vibration. A food processor cares about temperature and holding-tank conditions. Common signal types include:
- Machine states and cycle times
- Temperature, vibration, and pressure readings
- Energy consumption
- Quality parameters and process conditions
- Alarms and equipment events
Gateways and Connectivity
Mixed-vendor environments are the norm, not the exception. Gateways sit between machines and the monitoring platform, translating protocols, buffering data during network interruptions, and transmitting it securely upstream. This layer matters most in older facilities where equipment from five different manufacturers, spanning three decades, needs to speak the same language.
The Data and Analytics Layer
Raw telemetry becomes useful once it's stored, normalized, and tied to context: which machine, product, shift, and line produced it. Analytics then run trend analysis, anomaly detection, statistical process control, and OEE calculations.
A data historian keeps a permanent record teams can query later for root-cause work.
Dashboards, Alerts, and Response

Data only creates value once someone sees it and acts. Vistrian's Manufacturing Suite illustrates this approach. FactoryLOOK connects to machine controllers, logs, databases, and IIoT devices, then feeds that data into customizable, role-based dashboards. A rules engine flags anomalies as they happen.
Alert thresholds need calibration, though. Set them too loose and you miss real problems. Set them too tight and operators start ignoring notifications entirely, which defeats the purpose. Fewer, better alerts beat a flood of noise every time.
Essential IoT Monitoring Software Features for Manufacturing
Not every platform that calls itself "IoT monitoring" delivers what a plant floor actually needs. Here's what to check.
Real-Time Data and Connectivity
Teams need current machine status, output, downtime reasons, and process conditions in one place, not scattered across five systems. Strong connectivity means:
- Support for legacy controllers, including systems decades old
- Compatibility with mixed-vendor equipment and standard industrial protocols
- Ability to pull data from logs and databases when direct integration isn't possible
- IIoT sensor options for machines without digital interfaces
Alerts and Manufacturing Analytics
Threshold alerts and anomaly detection only matter if they connect to a person responsible for acting. Look for configurable escalation, not just a generic notification.
On the analytics side, Vorne's OEE framework breaks performance into three components: availability (run time divided by planned production time), performance (ideal cycle time times total pieces, divided by run time), and quality (good pieces divided by total pieces).
Vorne notes that 85% OEE is often treated as a top-tier benchmark, but a new baseline might sit at 60% or lower. Treat that number as a stretch goal, not a starting expectation.
Manufacturing analytics platforms should cover:
- OEE, availability, performance, and quality
- Throughput, utilization, yield, and cycle time
- Downtime and bottleneck analysis
- Statistical process control (SPC)
- Root-cause analysis

Maintenance and Asset Intelligence
Historical telemetry supports preventive, condition-based, and predictive maintenance, but these aren't interchangeable. Preventive maintenance runs on a calendar. Condition-based and predictive maintenance respond to actual equipment behavior—vibration trends, temperature drift, or alarm frequency.
VistrianMMS pairs with FactoryLOOK to pull machine, PLC, and sensor data directly into work orders. Alerts don't just notify; they trigger action with an owner and a due date attached.
Reporting, Security, and Scalability
Multi-site operations need consolidated visibility without losing plant-level detail. Priorities here include:
- Shift reports and historical comparisons
- Plant-to-plant benchmarking for enterprise leaders
- Role-based user permissions and secure data transmission
- Deployment flexibility across cloud and on-premises environments
- Integration paths to MES, ERP, and CMMS systems
Benefits and Manufacturing Use Cases
Connected monitoring pays off in ways that are easy to underestimate until you see them running.
Predictive and Condition-Based Maintenance
McKinsey documented a case where a manufacturer predicted roughly a quarter of equipment breakdowns with 85% accuracy, saving more than 10% per predicted event by avoiding overtime and rush parts shipping. That same case carried a 10% false-positive rate that added 1,000 extra maintenance cases annually, which erased much of the savings. Predictive maintenance works, but only with well-tuned models.
Condition-based monitoring delivers the same idea on the plant floor. At Blommer Chocolate, FactoryLOOK's historian tracked liquid-chocolate temperature continuously and flagged range violations in real time, protecting product quality before batches drifted out of spec.
Production Optimization
Vistrian's implementation at North America's largest cocoa processor extracted an average of 20 parameters per production tool at roughly one reading per second. That granularity let the team compare robotic-line behavior across shifts using event and alarm Pareto charts, identifying corrective actions within days rather than weeks.
The result, according to Thomas Bruguier of Blommer Chocolate:
"In our 50-year-old plant, Vistrian's FactoryLOOK application was able to provide insights to the causes of our production bottlenecks, increase our output potential and enabled us to avoid needless capital spending of over a million dollars."
Quality, Energy, and Multi-Plant Monitoring
- Quality monitoring: SPC and continuous process tracking catch deviations before they become recalls
- Energy monitoring: Connected meters reveal abnormal consumption patterns and efficiency opportunities across equipment
- Multi-plant monitoring: Centralized dashboards let operations leaders compare sites and standardize KPIs without visiting every location in person
Vistrian's Dashboards module, for instance, provides near-real-time views at the machine, line, plant, or enterprise level, giving leadership a single reference point instead of four different plant reports in four different formats.
How to Choose and Implement IoT Monitoring Software
Selecting a platform starts with a specific problem, not a feature checklist.
Start With a Measurable Goal
Pick one:
- Reduce unplanned downtime on a critical line
- Improve OEE visibility plant-wide
- Monitor a specific asset group at higher risk of failure
- Consolidate reporting across multiple plants
Audit Before You Buy
Before evaluating vendors, inventory what you actually have:
- Machines, controllers, and their ages
- Existing protocols and data sources
- Current MES, ERP, or CMMS tools
- Network conditions across the facility
- Who owns responding to alerts once they fire
Compare Platforms on Substance
Build a scorecard covering:
- Legacy-equipment support and connectivity depth
- Alert quality and escalation logic (not just alert volume)
- Deployment model: cloud, on-premises, or hybrid
- Integration with MES/ERP/CMMS
- Total cost of ownership, not just license price
Roll Out in Phases
Start with one line or one high-value use case. Validate data quality and adoption before expanding. Vistrian's implementation at the cocoa processor followed this path: FactoryLOOK launched at one of four plants first, with rollout to the remaining three planned within six months once the initial results held up.

Vistrian's Manufacturing Suite is built for that same path. It pairs equipment integration and IIoT connectivity with historian storage, analytics, and dashboards in a modular, cloud-enabled package.
Teams can start on a single line, then expand to multi-plant monitoring as data quality and adoption prove out.
Frequently Asked Questions
What is an IoT monitoring system?
An IoT monitoring system collects and analyzes data from connected devices, machines, sensors, and networks to track health, performance, and operating conditions. The goal is timely action on that data—maintenance, quality, and production decisions—not collection alone.
What does IoT monitoring software do?
IoT monitoring software collects device and machine data, then turns it into dashboards, analytics, anomaly detection, alerts, and reports. It also connects those insights to maintenance and production systems so teams can act.
How does IoT monitoring work in manufacturing?
Machines and sensors generate data that flows through gateways into a central platform. From there, dashboards, alerts, and analytics turn that raw information into maintenance actions and production insights.
What features should IoT monitoring software have?
Prioritize legacy and mixed-vendor interoperability, real-time dashboards, historical storage, configurable alerts, and manufacturing analytics. Also require solid security controls and integration with MES, ERP, or CMMS systems.
What is the difference between IoT monitoring and device monitoring?
Device monitoring checks whether individual sensors or gateways are online and functioning. IoT monitoring connects that data to plant-level production, quality, and maintenance outcomes.
How do manufacturers choose IoT monitoring software?
Start with a specific business goal, then score platforms on legacy-equipment compatibility, security, integration depth, usability, and scalability. Run a phased pilot before a full rollout.